If you’re in the business of maintaining heavy industrial equipment—think mining drills, pump shafts, or large engine cylinders—you know how critical a good bore welder is. As a supplier who’s spent 12 years walking clients through every model, I’ve seen firsthand that not all bore welders are built the same. Pick the wrong one, and you’re looking at uneven welds that crack under pressure, downtime that costs you thousands per hour, or even damage to the very part you’re trying to repair. Let’s break down the key differences between the three most common models our team works with daily: manual, semi-automatic, and automatic bore welders, so you can cut through the noise and pick what actually fits your operation. Bore Welder

First, let’s ground this in what a bore welder does, just to make sure we’re on the same page. Unlike standard MIG or TIG welders, a bore welder is designed specifically to repair cylindrical metal bores—whether that’s a worn cylinder wall on a hydraulic press, a gouge on a crankshaft journal, or a pitted bore in a large engine block. It aligns a welding head along the central axis of the cylinder, builds up material evenly, and can even process post-weld machining right on site. That last part is a huge win for operations that can’t afford to ship parts off for repair. Now, the differences between models start with how much control you, the operator, have over that welding process—and that ties directly to the size of your parts, the skill level of your team, and your downtime budget.
Let’s start with manual bore welders, the workhorse for small, low-volume jobs. When I first got into this industry, manual welders were all we had, and I still recommend them to clients who work on parts under 24 inches in diameter, or who only repair 5 to 10 parts a month. The core of a manual model is a rotating welding head you hold steady with a hand crank, adjusting speed and wire feed rate by hand. It’s simple: no fancy software, no auto-alignment, just you, the head, and a set of calipers to check your build-up. But here’s what makes it different from other models: it’s cheap, lightweight, and portable enough to fit in the back of a pickup. Last year, a mining contractor who only fixes small drill bit housings came to us with a $1,800 budget—way under what semi-automatic models cost. We set him up with a manual bore welder, and six months later he told us he’d repaired 12 parts, no issues. But there’s a catch: manual welders rely entirely on operator skill. Even the most veteran welder can only hold a consistent weld speed for so long. I’ve seen manual welds on a 20-inch hydraulic bore end up 1mm thinner on one side, which meant the client had to rework it—wasting both time and material. That’s why manual models are best for small, low-stakes jobs where a small margin of error is acceptable, and your team has at least a year of welding experience under their belt.
Next up, semi-automatic bore welders, the middle ground that’s taken over mid-sized industrial operations over the last 10 years. What sets these apart is that they remove the human error factor of constant speed adjustments: the welding head rotates at a set, consistent speed, and the wire feed rate is controlled by a small digital controller, not your hand. But you still do the heavy lifting for alignment. A semi-automatic model’s core components are fixed on a frame that clamps to the end of the bore; you line up the central axis with a spirit level, adjust the clamp tension to keep it steady, and input your parameters (like wire size and amperage) into a small screen. No more cranking by hand—you just press start, and the head does its job. The biggest advantage here is accuracy: semi-automatic welds have a tolerance of ±0.2mm, which is way better than manual’s ±0.5mm. That’s a game-changer for parts that need to fit tight tolerances, like pump shafts or engine cylinders. I once worked with a construction company that repairs 50 to 60 excavator hydraulic bores a month; they were using manual welders and seeing a 15% failure rate in the first three months post-repair. We swapped them to semi-automatic, and that failure rate dropped to less than 3%. The only downside? Semi-automatic models are heavier (around 250 pounds, vs. 80 for a manual) and can’t process bores larger than 60 inches. If you’re working on 80-inch mine mill cylinders, a semi won’t reach that far. Also, they still require an operator to monitor alignment mid-job—if the frame shifts, the weld will be off. So if your team is short on experienced welders, a semi-automatic model is a big upgrade, but only if your parts aren’t too large.
Then there’s the automatic bore welder, the heavy-duty workhorse for large-scale industrial operations. This is the model that’s built for bores 60 inches and up, like those in large turbines, marine engine cylinders, or mining mill shafts. What makes automatic models different from the other two is that they’re fully programmable: you input every parameter—weld speed, amperage, wire feed rate, and even the exact amount of material to build up—into a industrial-grade PLC controller, and the machine does the rest. Alignment is also automatic: the machine has laser sensors that adjust the frame position in real time if it shifts, so you don’t have to hold a spirit level for an hour. Last year, we delivered an automatic bore welder to a power plant that repairs 100+ turbine cylinder liners a year; their old semi-automatic model required two operators to work 12-hour shifts, and they were paying a third party $12,000 per liner repair. With the automatic model, one operator can run three machines at once, and internal repairs cost $4,500 per liner. That’s a massive ROI, but it comes at a cost: automatic bore welders start at $25,000, vs. $2,000 for manual and $8,000 for semi-automatic. They’re also bigger—some models take up 10 square feet of floor space—so if you don’t have a dedicated repair bay, you can’t easily move them to job sites. Another thing to note: automatic models aren’t better for small jobs. The programming time for a tiny 10-inch bore takes longer than just welding it manually, so you’d be paying for features you’ll never use. I always tell clients: if your monthly repair volume is under 20 parts, automatic is overkill. If it’s over 50, and you’re working on bores 40 inches or larger, it’s a no-brainer.
Wait, but there’s another key difference I didn’t mention earlier: the type of wire they use. Some manual and semi-automatic models use solid wire, while many automatic models use flux-cored wire. Solid wire is cheaper and easier to use for small jobs, but it doesn’t adhere as well to worn cast iron or steel, which is what most bores are made of. Flux-cored wire has a protective flux that prevents porosity (tiny gaps in the weld) when you’re welding in dusty, on-site conditions—something you can’t get with solid wire. That’s why automatic models, which are usually used for on-site large repairs, rely on flux-cored. But modern semi-automatic models now have options for both wire types, so you can switch based on the job. That’s a detail that trips up a lot of first-time buyers: they buy a semi-automatic with only solid wire capability, and then have to rent a machine when they need to repair a cast iron cylinder on site.
I also get a lot of questions about portable vs. stationary models. Manual and most semi-automatic models are portable—you can load them into a van and take them to a mine or construction site to repair parts without shipping them. Automatic models, however, are almost always stationary, built to stay in a repair bay because of their size and power requirements. If your team does a lot of on-site repairs, manual or semi-automatic is the way to go; if you only fix parts in a dedicated shop, automatic might make sense.
Let’s wrap this up with a quick breakdown to make it easy: manual for small, low-volume jobs; semi-automatic for mid-sized, mid-volume jobs; automatic for large, high-volume jobs. But the best model for you also depends on skill: if your team has only basic welding experience, avoid manual—even a semi-automatic is more forgiving. If you have a dedicated repair bay and large parts, automatic will save you money in the long run.
At the end of the day, choosing a bore welder isn’t just about picking the most expensive model or the one with the most features. It’s about matching the machine to your operation’s needs, not the other way around. If you’re tired of dealing with welds that fail, or paying third-party repair fees, we can walk you through what’s worked for other operations like yours. We don’t push the most expensive model just for the sale—we’ve seen too many clients buy an automatic when a manual would have sufficed, leaving them out thousands of dollars. Let’s talk through your monthly repair volume, the size of the parts you work on, and your team’s skill level, and we can find the right fit for you.
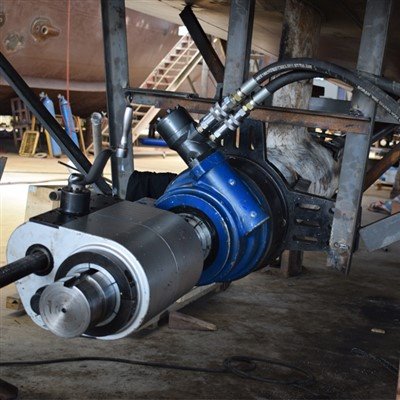
We specialize in bore welders tailored to industrial applications, and we offer on-site training and support to make sure your team gets up and running quickly. Whether you’re a small shop just starting out or a large industrial operation managing a fleet of heavy equipment, we have models that fit your budget and needs. Reach out to us to discuss your requirements, and we’ll help you find the right bore welder without the guesswork.
Line Boring References
- Industrial Welding Association. (2021). Guide to Cylinder Bore Repair Welding.
- Heavy Equipment Maintenance Journal. (2022). ROI of Automatic Bore Welding Systems for Industrial Operations.
- American Welding Society. (2020). Tolerance Standards for Bore Weld Repairs.
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional bore welder manufacturers and suppliers in China. We warmly welcome you to buy cheap bore welder for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
